

Smallest Air Compressor for Sandblasting: CFM & PSI Guide
Smallest Air Compressor for Sandblasting: CFM & PSI Guide

Quick Diagnosis: Air-Supply Symptoms
| What you see | Likely cause | Fix |
|---|---|---|
| Pressure drops while blasting | Worn nozzle (>20% bore), long/leaky hose | Check nozzle, shorten hose, fix leaks |
| Compressor cycles on/off | Duty-cycle limit, tank too small | Bigger tank / lower CFM draw |
| "Air but no sand" | CFM too low for the nozzle | Downsize nozzle or upgrade compressor |
| Water in media / rust inside | No moisture separator / clogged drain | Install & drain separator daily |
| Multi-station pressure sag | Shared shop air insufficient | Dedicated line or larger compressor |
| Overheats & shuts down | Reciprocating duty cycle exceeded | Two-stage / larger pump |
How Much PSI & CFM Do You Actually Need?
Pressure pots typically run 90–100 PSI at the nozzle; suction (siphon) cabinets about 60–80 PSI. But PSI is what the gauge shows — CFM is what the nozzle consumes. A compressor holding 100 PSI that can only deliver 5 CFM will collapse the moment you pull the trigger on anything larger than a 3/32 in nozzle. Size the machine to CFM first, PSI second.
Nozzle Size → Required CFM (at ~100 PSI)
These are typical values for a pressure-blast venturi nozzle. Exact numbers move with pressure and media, but the shape of the curve is what matters: CFM rises roughly with the square of nozzle diameter. Double the nozzle, you don't double the air — you multiply it.
| Nozzle | CFM @ 100 PSI | Smallest practical compressor |
|---|---|---|
| 3/32 in (2.4 mm) | ~12 CFM | 5 HP / 20–30 gal (intermittent) |
| 1/8 in (3.2 mm) | ~24 CFM | 5–7.5 HP / 30–60 gal, 2-stage |
| 5/32 in (4.0 mm) | ~38 CFM | 7.5–10 HP / 60–80 gal |
| 3/16 in (4.8 mm) | ~52 CFM | 10 HP / 80 gal, continuous |
| 1/4 in (6.4 mm) | ~95 CFM | 15–20 HP / 120 gal, rotary or large recip |
| 5/16 in (7.9 mm) | ~145 CFM | 25 HP+ / dedicated plant air |
The 9 Air-Supply Problems (and the Field Fix for Each)
1. Pressure drops while blasting
You see: pressure gauge sinks the second you pull the trigger. Root cause: worn nozzle (bore up 20%+), hose too long/thin, or leaks at fittings. Fix: measure nozzle bore, shorten and upsize the hose, soap-test fittings. A 20% bore increase can cut blasting efficiency by a third.
2. Airflow cycles on and off
You see: compressor kicks on, you blast a few seconds, it stops, repeats. Root cause: duty-cycle limit or undersized tank. Fix: add a secondary tank, or drop to a smaller nozzle so draw stays under the duty cycle.
3. Small compressor "won't drive it" — air but no sand
You see: air blows, but media never feeds. Root cause: CFM too low for the nozzle — pressure exists, volume doesn't. Fix: this is a sizing problem, not a machine defect. Down-size the nozzle or upgrade the compressor (see small-compressor fixes below). If media still won't feed with good air, the fault moved to the sand circuit — see the no-sand guide.
4. Water in the tank / media
You see: moisture in the line, abrasive clumps, nozzle rusts. Root cause: no moisture separator or never drained. Fix: install a dryer/separator and drain the tank and separator every shift. This single habit prevents most "clog" calls.
5. Shop air can't keep up (multi-station)
You see: pressure sags when a second blaster or tool starts. Root cause: shared line undersized for total CFM. Fix: run a dedicated line to the blast cabinet, or size the compressor for peak combined demand + 30% margin.
6. Duty cycle exceeded → overheating
You see: reciprocating compressor gets hot and trips. Root cause: continuous blast exceeds the pump's duty cycle (often 50–60%). Fix: two-stage pump, larger tank buffer, or a rotary-screw unit for production use.
7. Tank too small
You see: short blasts OK, sustained work fails. Root cause: <60 gal can't buffer CFM swings. Fix: add a 60–120 gal auxiliary tank; it smooths demand so the pump doesn't hunt.
8. Media too heavy for the air
You see: steel grit/steel shot won't move on a small source. Root cause: dense media needs more CFM to convey. Fix: switch to lighter media (glass bead, garnet, plastic) for small setups, or step up compressor CFM for steel media.
9. Wrong attachment / plumbing
You see: rigged a pot to the compressor but it pulses or won't feed. Root cause: no regulator, no moisture control, wrong coupling. Fix: use a proper metering valve and regulator; don't T a pot straight off the tank. See the attachments section below.
Small-Compressor Fixes — Make a Small Unit Work
If you're stuck with a smaller compressor, these are the field-proven ways to get effective results instead of buying a bigger machine:
✔Drop the nozzle: a 3/32 in nozzle needs ~12 CFM vs ~95 for a 1/4 in — the single biggest lever.
✔Add an auxiliary tank (60–120 gal) to buffer demand and stop the pump hunting.
✔Switch to a siphon/suction cabinet or a pressure pot at lower PSI — both sip less air than a wide-open pressure blast.
✔Use lighter media: glass bead or garnet conveys on far less CFM than steel grit/steel shot.
✔Lower working pressure 10–15% and accept a slower cut — often enough for cleanup and coating prep.
✔Pulse-clean and dry the air: moisture in the line costs you effective CFM more than people realize.
Full low-CFM technique breakdown: Low-CFM Sandblasting: How to Get Effective Results.
Sandblaster Attachments That Work With an Air Compressor
Yes — most blasters are air-compressor attachments by definition. What matters is matching the type to your compressor's CFM:
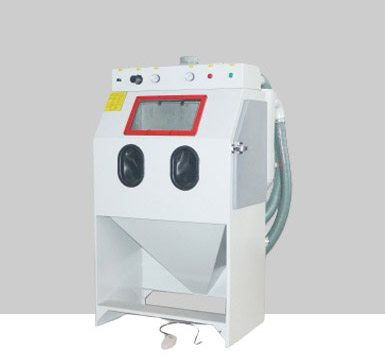
✔Suction / siphon blaster (cabinet or handheld): runs off any standard compressor; lowest CFM demand. Best first buy.
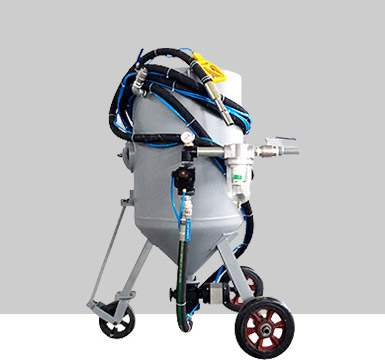
✔Pressure pot blaster: connects through a regulator + metering valve; higher throughput, needs more CFM.
✔Venturi nozzle: the standard nozzle that converts pressure into conveyance velocity — size it to your CFM, not your hopes.
✔What to avoid: plumbing a pot straight off the compressor outlet with no regulator, dryer or metering valve. That's the #1 cause of pulsing and clogs.
Separator
Pot
Nozzle
How to Size Your Compressor (Quick Method)
Step 1 — pick your nozzle for the job (bigger = faster but thirstier). Step 2 — read its CFM from the chart above. Step 3 — add 25–30% margin for wear, altitude and aging. Step 4 — size the tank to ~1 gallon per 1 CFM of draw, minimum 30 gal for any sustained work. Step 5 — verify duty cycle covers continuous runtime.
Full nozzle CFM reference: How Much CFM Does a Sandblast Cabinet Need? (complete chart).
Air-System Preventive Maintenance
✔Drain compressor tank and moisture separator every shift — non-negotiable.
✔Fit a dryer/separator before the pot; replace filter elements on schedule.
✔Inspect hoses and couplers for leaks; a small hiss is lost CFM.
✔Keep hose runs short and wide-bore to protect working pressure at the nozzle.
✔Log nozzle bore; replace at +20% to protect both pressure and media spend.
✔Size the dedicated air line to the cabinet, not shared with random shop tools.
More field tips: 10 Sandblasting Tips & Tricks.
Frequently Asked Questions
When to Call the Manufacturer
Air-side issues above are usually field-fixable. Contact TS Blasting when you're specifying a new line and need the compressor matched to throughput, when recurring pressure loss points to a worn pot or liner, or when you want a free sample blast to prove the setup before you buy.
Free Sample Blast & Air-System Sizing
Not sure which nozzle, media and compressor combo fits your job? TS Blasting runs a free sample blast on your part and gives you a free air-system specification — 18 years and 30+ country field data behind it.
Request a Free Sample TestBack to Air-Supply Guide